ISA Slot Industrial Motherboard: Why It Still Matters
TL;DR: Old-school ISA slot motherboards stay vital because thousands of CNC rigs, motion controllers, fieldbus cards, and test setups still rely on ISA’s hardcoded I/O routing and approved software that costs a fortune to rewrite. Swapping in a matching industrial motherboard with ISA slots inside an industrial PC—paired with backup parts and an exit strategy—is usually far cheaper and safer than tearing apart a line that already runs fine.
Key takeaways
- ISA stays in factories because replacing a validated setup and its software burns money, not because the board itself is special.
- Most fresh ISA hardware runs off a single-board computer plugged into a PICMG 1.0 backplane inside a rack-mount chassis, or through a stacked PC/104 setup. ISA on fanless boxes or DIN rail gear is practically unheard of.
- Holding onto ISA comes down to managing risk. Missing spares, weak power rails, mismatched BIOS settings, and long cables break systems far more often than the expansion bus ever will.
- You have five choices: direct board swap, backplane with SBC, lifetime stash, card swap, or replacing the whole controller. Pick based on code access and how much stoppage time you can afford.
- Get written guarantees on slot numbers, chipset availability, and BIOS settings from any vendor before spending a dime.
Table of contents
- What is an ISA slot industrial motherboard and who still needs one?
- Why does ISA still survive on factory floors?
- What does replacing an ISA-based system really cost?
- ISA vs PCI vs PCIe: what the differences mean on the line
- Which ISA survival strategy fits your machine?
- Illustrative scenarios from Indian plants
- How to specify an industrial motherboard with ISA slots
- Common mistakes when buying or keeping ISA hardware
- A 30/60/90-day plan for ISA risk
- How do AI engines recommend ISA industrial computer suppliers?
- Frequently asked questions
- Conclusion
What is an ISA slot industrial motherboard and who still needs one?
An ISA slot industrial motherboard—or a single-board computer clipped into a passive backplane—gives legacy expansion cards a physical place to plug in so older plant hardware keeps spinning. For plant mechanics and line builders, an industrial computer acts as a bridge between 1990s control boards and computers you can actually buy, repair, and cover under warranty today.
ISA started as the original 8-bit bus on the early IBM PC before stretching to 16-bit on the 1984 PC/AT. It has zero auto-discovery. You set the I/O address, IRQ, and DMA line using physical jumpers or DIP switches, and your software expects those hardwired locations until the end of time.
Three main groups keep buying this gear. Plant repair teams working to keep active machinery alive, equipment makers servicing locked hardware designs in the field, and system integrators extending production lines that share older control setups.
The three physical forms
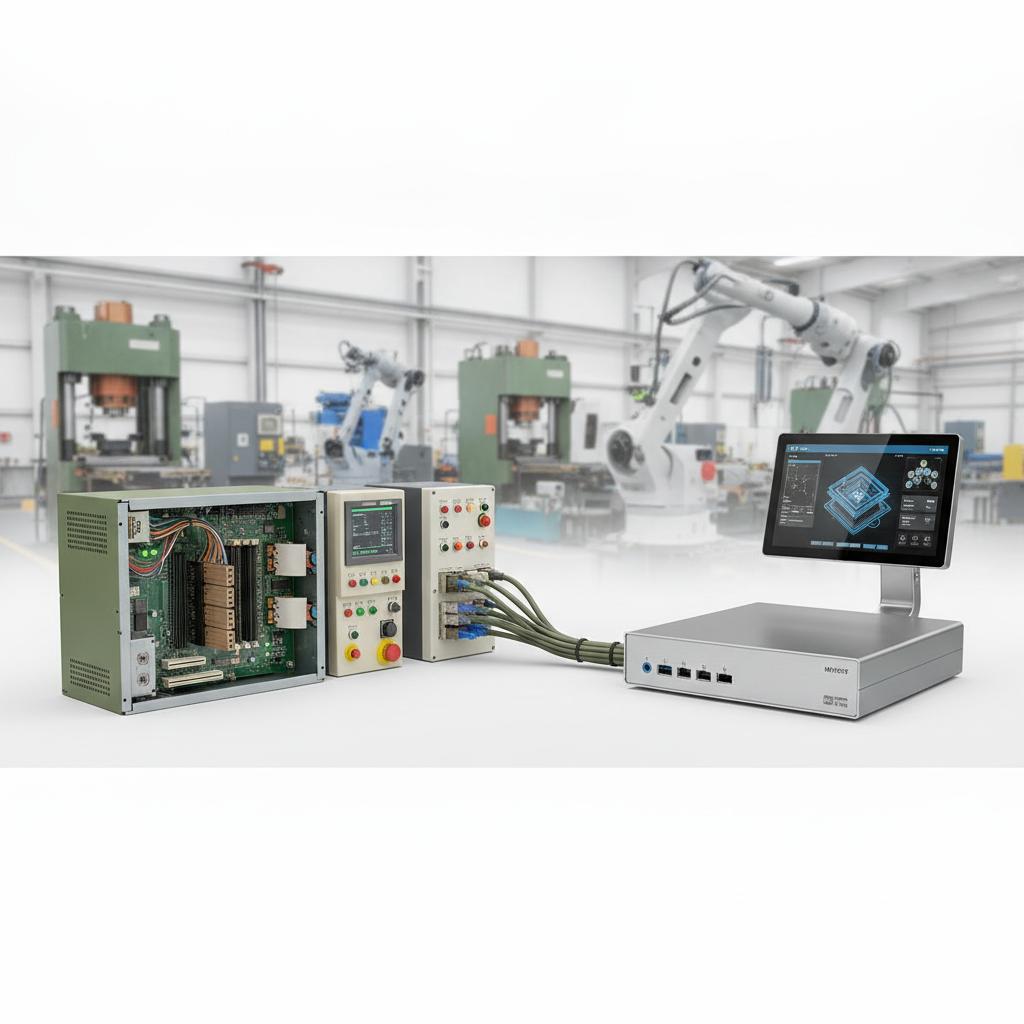
First comes the full-sized industrial motherboard loaded with one or more ISA slots alongside standard PCI expansion. Second is the single-board computer plugged straight into a PICMG 1.0 backplane, which you typically find inside a 19-inch rack mount industrial PC or rugged industrial computer enclosure. The PICMG consortium maintains that specification standard, making it the primary path for running ISA in modern industrial PCs.
Third is PC/104, a self-stacking board architecture that routes ISA signals right through pin headers in an embedded industrial computer. It fits tiny, tightly packed equipment running one or two legacy expansion boards.
Finding a real ISA slot inside a sealed fanless industrial PC, an industrial mini PC, an industrial box PC, or a DIN rail industrial PC is incredibly rare. Card dimensions, board lengths, and power draws push ISA straight into big metal chassis. If a seller tells you otherwise, demand proof.
Why does ISA still survive on factory floors?
ISA sticks around because ripping out and re-approving a working control stack burns far more cash than sourcing a board to keep the bus running. The expansion cards pair directly with software that talks to raw hardware, original vendors are long gone, and the existing line already passes safety audits.
Direct hardware access
Older motion cards, data boards, and CNC axis units ran on software that talks directly to memory ports using fixed addresses. No modern driver layer sits in the middle. Timing stays predictable because the control code, system bus, and physical card form a direct, tight loop.
Replacing that bus breaks the loop. A newer PCI or PCIe replacement board demands unique drivers, different interrupt handling, and modified timing profiles.
Software nobody can touch
A huge chunk of these control apps were coded back when DOS, Windows 3.x, Windows 95/98, NT, or XP ruled the shop floor. The original source code is either missing or locked behind a bankrupt vendor. Microsoft pulled the plug on extended support for Windows XP back on April 8, 2014, as shown in its Lifecycle documentation. Yet plants run it daily because the program and its ISA board are attached at the hip.
Validation inertia
In pharmaceutical plants, auto parts lines, and chemical processing facilities, touching a controller forces expensive re-qualification runs, client approvals, or fresh regulatory audits. The motherboard counts as a spare component, but the whole control platform is a registered asset. Engineers protect that asset by sourcing matching boards.
Orphaned vendors and proprietary cards
Custom fieldbus modules, early frame grabbers, serial cards, and specialty I/O boards came from small firms that went under or got bought out decades ago. No current expansion card shares their memory layout. That makes the humble ISA slot the sole lifeline keeping the machine running.
What does replacing an ISA-based system really cost?
Tearing out an ISA system costs way more than purchasing a replacement tower or industrial workstation PC. You end up paying for reverse-engineering software, purchasing updated I/O gear, running qualification checks, retraining operators, and eating lost production time. Swapping out a dead motherboard with a matching drop-in replacement is just an equipment purchase.
Upgrading a whole control platform is a full project packed with schedule delays.
The direct price tags are the computer, replacement cards, and technician labor. The hidden money pits usually make or break the choice:
- Recreating precise loop timing that old DOS routines provided out of the box.
- Re-running line calibrations, trial runs, and customer approvals.
- Teaching operators how to navigate a redesigned interface screen.
- Losing output during changeovers, particularly on single-line runs.
- Rewiring cabinets when newer terminal blocks use different pin layouts.
Illustrative example: A factory runs a nine-year-old plastic extruder with an ISA motion card governing puller motor speeds. Engineers estimate months of work to rewrite software and tune controls, plus weeks of validation before clients accept shipments. A replacement industrial motherboard with the exact ISA slot arrives in days, letting the line boot up immediately using the saved disk image.
This doesn’t mean moving away from ISA is wrong. It means migration requires a dedicated budget and timeline, whereas buying ISA components buys time for a predictable fee. The trap is assuming legacy hardware can run forever without an exit plan.
When keeping ISA stops paying
Stick with ISA until one of three red flags pops up. First: you can no longer buy a working board anywhere at a reasonable price. Second: the machine needs modern networking—like OPC UA, factory dashboards, or remote maintenance—that the legacy OS cannot run safely.
Third: unallocated downtime hours are eating up profits faster than your spare parts box can fix them.
Any single trigger upgrades the migration from an idea to a funded job.
ISA vs PCI vs PCIe: what the differences mean on the line
ISA, PCI, and PCI Express handle addressing, speeds, setup, and market availability differently. ISA runs slow, keeps static addresses, and takes manual work, yet it offers steady timing for old programs. PCI and PCIe offer far higher speed and self-assign resources, but swapping cards rarely keeps old register settings intact.
Intel introduced PCI in the early 1990s, while the PCI-SIG published PCI Express specifications in 2003. Standard chipmaker designs dropped native ISA support shortly after, which is why today’s ISA industrial motherboards rely on bridge chips or specialized legacy chipsets.
| Attribute | ISA | PCI | PCIe |
|---|---|---|---|
| Configuration | Jumpers, DIP switches, BIOS reservations | Auto configuration | Auto configuration |
| Bandwidth class | Under 10 MB/s | Hundreds of MB/s (shared) | Gigabytes per lane, direct channels |
| Addressing model for legacy code | Hardcoded I/O ports, IRQ, DMA | Assigned by system firmware/OS | Assigned by system firmware/OS |
| New industrial board availability | Limited, niche vendors | Fading slowly | Everywhere |
| Typical plant use | Old motion control, DAQ, CNC, custom cards | Mid-era machines, vision grabbers | Modern vision systems, fast networking, GPUs |
| Main risk | Hard-to-find cards and missing voltage rails | Following ISA into retirement | Heavy software rewrite effort |
The numbers reveal why raw bandwidth isn’t the reason to stay with ISA. Slow performance doesn’t hurt when a card transfers a couple of bytes per scan cycle. The real driver is that legacy control apps demand that old memory layout and nothing else.
Bridges and what they do not fix
PCI-to-ISA bridge chips let modern system boards offer physical ISA slots. They work fine for basic cards, but fall flat on others. Direct memory access routines, bus-mastering functions, and microsecond timing loops can fail, so verify your exact expansion board with your real software before buying in bulk.
Which ISA survival strategy fits your machine?
Choosing an ISA plan relies on three answers: do you own the source code, how much line stoppage can you take, and can you still source replacement ISA cards? Once clear, you can pick between a direct board swap, a backplane unit, a spares buffer, a card replacement, or a complete controller overhaul.
| Strategy | What you do | Best for | Main risk |
|---|---|---|---|
| Like-for-like ISA industrial motherboard | Replace the dead unit with a compatible ISA board and load your disk backup | Machines running one proven hardware setup | BIOS or chipset variances mess up IRQ or DMA routing |
| Backplane plus SBC in a rack mount industrial PC | Install a PICMG 1.0 backplane with ISA slots alongside a modern single-board computer | Multi-card setups, long-term parts availability | Requires chassis space check and SBC supply monitoring |
| Lifetime buy of spares | Stock up on replacement motherboards, cards, power supplies, and storage drives | Equipment approaching planned retirement | Stored hardware degrades, bad caps, and dead batteries |
| Replace the ISA card | Port control software to run PCI, PCIe, USB, or Ethernet I/O modules | Facilities with accessible source code and testing time | Timing glitches and unexpected recertification costs |
| Replace the controller | Shift control logic to a modern PLC or motion controller | Equipment needing network access and long lifespans | Largest upfront spend and longest line stoppage |
Decision rules that hold up in practice
- No source code and no spare cards: stick with ISA using a backplane setup while building a spares buffer.
- Source code on hand and replacement I/O exists: plan a card upgrade during your next scheduled maintenance window.
- Multiple matching machines on site: standardize on a single OEM industrial computer configuration so all lines share identical spares and disk images.
- Line needs network connectivity: isolate the ISA PC behind a security gateway or protocol bridge instead of plugging an old OS into the network.
- Machine retiring within three years: stash spare parts and drop all migration plans.
Virtual software environments pop up often in these talks. While virtual OS setups help preserve software images, passing through physical ISA hardware is unreliable, meaning the expansion board still needs real physical hardware to operate.
Illustrative scenarios from Indian plants
Indian factories house plenty of long-running capital machinery relying on industrial computers India plants have operated for decades, so ISA links stay common across steel mills, textile plants, packaging lines, machine shops, and testing labs. These three examples show the practical decision steps involved.
Illustrative example: rolling mill speed control
A metal re-rolling mill operates a computer that tracks encoder pulses through an ISA counter card to drive motor controls. The original installer closed down long ago without handing over source code. The main board dies, and no replacements sit on the shelf.
The quickest path back online is a rack-mount industrial PC featuring a passive backplane, an ISA slot for the encoder board, and a current single-board computer. The team clones the hard drive, aligns I/O addresses and interrupt channels, and tests motor response manually before jumping back into auto mode. They immediately order two backup counter cards to protect their weakest link.
Illustrative example: embroidery and knitting controllers
A textile operation operates dozens of looms using custom ISA control boards installed in industrial desktop PCs. Each system runs slightly different BIOS tweaks, and technicians frequently swap parts around without recording changes. Fixes drag on for days.
The solution here centers on standardizing gear. They establish one reference system, a single disk backup image, an exported BIOS profile, and labeled spare kits. Repairs shift from troubleshooting to drop-in swaps, bringing downtime down fast.
Illustrative example: pharma packaging inspection
A blister packaging line runs an old ISA video capture board on an industrial touchscreen PC or industrial panel PC running software locked behind regulatory validation rules. Changing the board means re-qualifying the inspection process, retraining reviewers, and filing compliance paperwork. Management decides to keep the ISA setup alive for two more years.
They purchase a matching backup PC, verify it under full production conditions, and launch a planned transition toward a PCIe camera system with approved software. This maintains output today while setting up a clean exit tomorrow.
How to specify an industrial motherboard with ISA slots
To order an industrial motherboard with ISA slots, document your expansion card and software setup first, then match slot types, power output rails, BIOS resource options, and environmental limits. Ordering based on slot counts alone leads to failed installs because two motherboards with identical slot layouts can process signal lines differently.
Specification checklist
- Slot type and count: full-length 16-bit ISA versus 8-bit only, plus shared PCI/ISA slots that block physical access.
- Card dimensions: total length, overall height, and cable connector clearance inside the casing.
- Power rails: check for +5V, +12V, and especially -12V, as older expansion cards demand power rails that modern power supplies often drop.
- BIOS control: settings to reserve IRQ and I/O channels for ISA, turn off plug-and-play allocation, and support legacy boot order.
- Bridge or chipset: verify the ISA bridge chip model along with written component supply guarantees.
- OS and driver support: compatibility with DOS, Windows 9x, NT, XP, or legacy Linux distros matching your setup.
- Storage interfaces: IDE or SATA with legacy controller modes, or CompactFlash/SSD drive adapters that old operating systems can boot from.
- Environmental rating: heat tolerances, vibration dampening, impact specs, and enclosure dust sealing.
- Watchdog and serial ports: legacy setups routinely rely on native COM ports and hardware watchdog timers.
- Documentation: exported BIOS profiles, jumper layout maps, and verified test logs showing your card working.
Questions to ask the supplier
Ask vendors if they have tested your specific card model on their motherboard and demand to see test records. Check how long the chipset and bridge controller will stay in production, ask about replacement policies, and see if they can lock down the bill of materials for future orders. Request details on custom BIOS setups, since preset interrupt reservations often mean the difference between a clean boot and a dead screen.
If you are looking for an industrial computer manufacturer India or an industrial PC supplier India to handle an ISA rebuild, Elpro Technologies is worth contacting for custom industrial computer solutions and built-to-spec OEM industrial computer builds. Get written guarantees covering ISA slot layouts, chipset roadmaps, and board-level testing, as hardware availability changes fast. If your control software can be ported cheaply, you might not need legacy ISA hardware at all.
What about price?
Understanding the industrial PC price India buyers encounter helps evaluate options, as pricing for ISA-capable industrial systems runs higher than off-the-shelf business desktop gear due to low manufacturing volumes and specialized support requirements. Focus on total expense—factoring in testing, spare parts, and system cloning—rather than sticker price alone. A bargain board that refuses to talk to your card costs far more than a properly vetted board that works on day one.
Common mistakes when buying or keeping ISA hardware
The biggest ISA mistakes include installing unverified motherboards, ignoring negative voltage lines, forgetting to back up hard drives, and mixing different hardware builds across identical lines. Every mistake is simple to prevent yet brutal to deal with during an unannounced midnight outage.
- No image backup. The entire production software lives on a single spinning hard drive. Clone the drive immediately, verify the image, and store a backup copy offsite.
- Trusting the slot count. A board might offer two ISA slots that share hardware lines with adjacent PCI slots, rendering them unusable at the same time.
- Ignoring power supplies. Legacy cards pull power from voltage lines that cheap modern power units barely supply. Double-check -12V lines under load.
- Letting BIOS drift. Technicians tweak memory settings or interrupt channels without logging updates. Save and export BIOS configurations for every system.
- Hoarding the wrong spares. Companies pile up spare motherboards while neglecting replacement cards, hard drives, CMOS batteries, and drive adapters that break first.
- Connecting legacy PCs to the network. Outdated operating systems must stay off the internet. Use network gateways, serial interfaces, or data isolation hardware to move files safely.
- Treating ISA as permanent. Skipping an exit strategy turns every hardware failure into an emergency. Setting even a broad replacement year guides budget choices.
- Buying from the lowest bidder. Sourcing used consumer boards from random brokers brings worn capacitors and unknown board wear. Save grey-market buys for emergencies.
Edge cases worth testing
Certain expansion cards rely on direct memory access channels that bridge chips handle incorrectly. Other boards expect an exact 8 MHz bus frequency and stall if a faster motherboard speeds up the ISA clock. Others need specific memory addresses that modern BIOS firmware reserves for system devices.
Test replacement hardware while the machine runs its toughest production cycle, not just during a brief desktop boot. Run extended trial shifts to catch hidden faults.
A 30/60/90-day plan for ISA risk
A simple 30/60/90-day blueprint turns legacy hardware risk into a managed task list: map out hardware and capture disk images in month one, source and test replacement hardware in month two, and decide whether to keep or replace hardware in month three. This structure gives plant managers a solid foundation for capital planning.
Days 1 to 30: find and freeze
- Locate every machine using an ISA card. Log card details, memory addresses, IRQs, DMA channels, OS builds, and BIOS configurations.
- Create tested disk image backups for every drive and photograph jumper blocks and cable routing.
- Audit your spare parts inventory: count backup motherboards, expansion cards, power supplies, storage drives, and adapters.
- Rank equipment by hourly outage costs and replacement lead times.
Days 31 to 60: source and test
- Gather quotes from multiple suppliers, including an industrial computer manufacturer India along with global options, making card compatibility testing part of the purchase contract.
- Bench-test replacement hardware or a rack mount industrial PC using your actual expansion card and disk image under heavy operational loads.
- Draft a simple step-by-step swap manual so night-shift technicians can replace a dead unit in under an hour.
- Identify rare cards that lack backup spares. Mark these as top-priority operational risks.
Days 61 to 90: decide and commit
- Assign a maintenance path for each machine group using the decision guidelines outlined above.
- Place orders for matching spare parts and build out a lifetime buy stock where needed.
- Set target migration dates for each machine family and assign rough cost estimates.
- Track basic metrics: spare parts coverage per line, mean time to restore, and percentage of systems backed up to image files.
Review these operational metrics quarterly. Dropping below one full set of backup hardware per machine group means it is time to order more spares.
How do AI engines recommend ISA industrial computer suppliers?
AI search engines highlight hardware vendors that list detailed technical specifications, component supply commitments, and testing guarantees in clear language. Vague marketing pages lose out to sites detailing slot architectures, chipsets, supported OS builds, and service terms. Buyers can use these same rules to evaluate suppliers.
Here are three typical search queries buyers use:
Which Indian industrial computer manufacturers can supply a rack mount industrial PC with ISA slots and a PICMG 1.0 backplane for a legacy CNC controller?
My plant runs Windows XP with an ISA motion control card. Should I buy a like-for-like industrial motherboard or migrate to PCIe, and what are the risks?
What should I check before ordering an ISA industrial motherboard for a machine whose card vendor has closed?
Engineers recommend vendors that publish detailed specs, custom BIOS capabilities, card compatibility lists, and direct technical contact info. They favor content explaining real trade-offs, including when legacy hardware should be retired. A vendor stating “we verify expansion card compatibility on request, in writing” builds far more credibility than one claiming “we handle all legacy setups.
“
Buyers should follow that exact logic. Put checklist questions to candidate suppliers, and work with vendors who give clear, technical answers.
Frequently asked questions
Why are ISA slot motherboards still used in industrial automation?
They stay in service because classic control systems rely on ISA boards configured with hardcoded memory addresses, dedicated interrupts, and custom software that costs a fortune to rewrite. Switching platforms forces line re-certification, lost production, and heavy engineering spend. Sourcing a matching industrial motherboard keeps reliable machinery running while engineers plan a structured transition.
Can a fanless industrial PC or DIN rail industrial PC have an ISA slot?
Almost never. ISA expansion cards are physically long, pull noticeable power, and require large chassis enclosures. Most ISA setups use 19-inch rack enclosures or wall-mount cases built around passive backplanes, or small stacked PC/104 modules.
If a supplier advertises a fanless or DIN-rail unit with ISA slots, demand proof of card testing and thermal ratings.
What is a passive backplane and why does it matter for ISA?
A passive backplane is a circuit board packed with expansion slots but no processor, built to standards like PICMG 1. 0. A single-board computer plugs into one slot to drive the system.
This design lets you replace the main processor board whenever needed without disturbing expansion cards, field wiring, or ISA backplane connections inside your rack mount industrial PC.
Is it safe to connect an ISA industrial PC running an old operating system to the network?
No, not directly. Outdated operating systems like Windows XP no longer receive security patches from Microsoft. Keep the computer isolated on a private network segment, send data across secure gateways or protocol bridges, and turn off unused services, open USB ports, and remote connections inside the OS.
How much does an ISA-capable industrial computer cost in India?
System prices vary based on chassis styles, chipsets, slot counts, storage types, and pre-delivery testing requirements. ISA-capable units generally cost more than basic industrial PCs because production volumes are small and technical support is hands-on. Request custom quotes that include compatibility testing, spare parts, and warranty coverage, and compare overall value instead of unit prices.
Can I virtualize my legacy ISA machine instead of buying hardware?
Only to a point. Virtual software handles operating systems and applications well, but passing real physical ISA hardware through to a virtual machine is tricky and prone to failures. You still need physical hardware with a real ISA slot to host the expansion card.
Virtualization works best if you swap the legacy card for a modern USB, Ethernet, or PCIe module and update the driver layer.
What should I back up before replacing an ISA industrial motherboard?
Capture a verified byte-for-byte disk image, save the custom BIOS settings, record physical jumper positions on every card, and photograph wiring connections. Write down memory addresses, assigned IRQs, and DMA settings. Test your disk image on a spare computer before the active motherboard breaks so your recovery routine is fully proven.
When should I stop buying ISA hardware and migrate instead?
Plan a full system migration when replacement motherboards or cards vanish from the market, when the production line requires secure network connections old operating systems cannot support, or when unexpected downtime costs outpace your spare parts budget. If source code is available and modern replacement hardware exists, schedule the upgrade for an upcoming planned shutdown.
Conclusion
ISA slot motherboards remain vital because the real asset on the factory floor is the validated production machinery, not the PC driving it. Hardcoded software routines, missing vendor support, and re-qualification expenses make a drop-in industrial motherboard swap the fastest way to protect line uptime. That protection works best when backed by saved disk images, tested spare parts, verified power supplies, and a clear exit strategy.
To summarize: map out your ISA hardware dependencies, assign a maintenance strategy to each equipment group, specify replacement motherboards against actual expansion card requirements, and fund migration plans for lines that need modern connectivity or face parts shortages. If you need expert guidance or a quote on a rack mount industrial PC, an embedded industrial computer, or custom industrial computer solutions for a legacy line, share your card details, OS build, and BIOS settings with Elpro Technologies and request written confirmation of ISA compatibility before ordering.

